
Stamping is the process of shaping flat metal with a die and a punch, and in watchmaking it is the quick, high-volume first step for parts that start as sheet or strip. A steel die, shaped like the finished part, shears, bends or presses the metal in a single stroke. Everything that makes the part look finished comes afterward, so stamping makes the shape and the later operations make the watch.

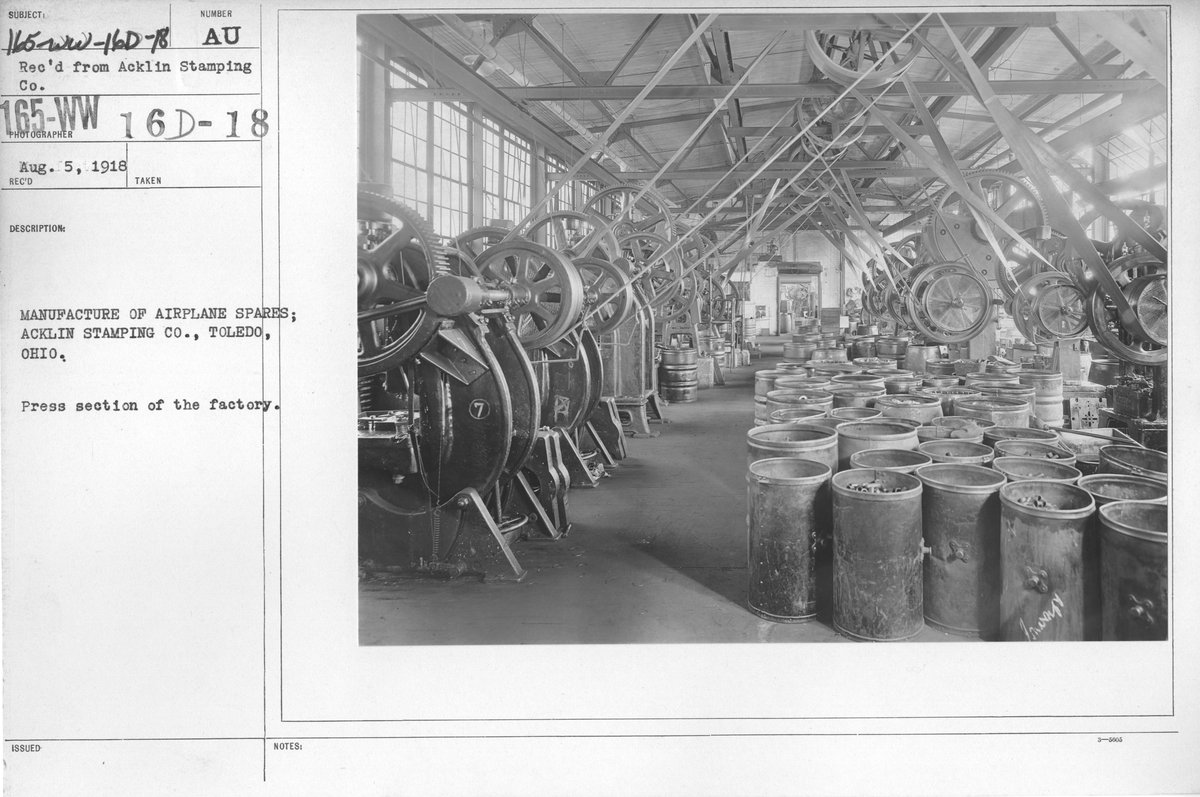
A 1945 eccentric press. The flywheel stores energy between strokes; the die does the actual shaping. Photo: Wikimedia Commons, GFDL 1.3.
How it works
A watchmaking stamp is a steel die, the hollowed negative of the part, paired with a punch, the matching positive shape. Three operations do the work: punching cuts the part out of the material, stamping forms a shape or pattern, and bending shapes the material without cutting it. Punching is shearing. The punch pushes into the sheet until the metal around the edge fails in shear, and the clearance between punch and die, a small fraction of the sheet thickness, sets the quality of the edge: too tight wears the tool, too loose leaves a burr. The force needed is the shear strength of the metal times the cut perimeter times the thickness.
The parts include movement components (wheels, springs and pallets) and case components (cases, dials and bracelets), in gold, platinum, steels, brass and aluminum. Presses range from manually operated screw presses, which apply a few hundred kilograms to several tonnes of force, to hydraulic presses reaching 1 to 200 tonnes. Stamps are costly to make because they are handmade, but the cost per part drops with volume and dies can last decades. Stamping also leaves stress in the metal, so annealing is needed afterward. Stamping declined after 1980 but has recovered, because CNC machines now make dies more cheaply.
Progressive dies
For high volumes, factories use progressive dies. A continuous metal strip advances a fixed distance, the feed pitch, with each press stroke. The die is divided into stations, each performing one operation on a different section of the strip, and each stroke completes a step at every station at once. Typical dies have 4 to 30 stations. The part stays attached to a carrier strip until the end, when it is cut free. Conical pilot pins enter pre-punched holes to correct small feed errors and keep each station aligned.
The operations are blanking (cutting the outline from the strip), piercing (punching holes), forming (bending, drawing or embossing in steps) and coining (pressing the metal to shape fine surface features). Production rates of 7 to 1,500 parts per minute are cited, depending on the part, and tolerances of about ±0.025 mm maintained across long runs. These are general sheet-metal figures, not watch-specific ones.
Dials and cases
One in-house dial process shows where stamping sits in a modern dial. Blanks are punched from brass, German silver or other metals to tolerances of a few hundredths of a millimeter. Computer-controlled milling then cuts openings for date windows and sub-dials, the blank is trimmed to final diameter, and dial feet are attached by friction fit or laser welding. Surface treatment, pad printing, applied markers and luminous elements follow, and each dial goes through up to 75 process steps.
For cases, TAG Heuer’s description of its Cornol workshop makes stamping the first of four stages (stamping, machining, polishing, assembly). Stainless steel or titanium sheets are cut into rough case shapes, which the article calls metal discs. Complex pieces need up to 16 operations between the raw bar and the basic shape, each disc is pressed with 70 tonnes of pressure, and the discs are annealed to relieve stress. These blanks are then refined by machining and polishing.

Stamping discs from steel strip on a punch press, photographed in the 1940s. The process has barely changed; the presses just got faster. Photo: Wikimedia Commons, public domain.
Sources
- “Stamping Presses,” Horopedia
- “Progressive Die Stamping,” Xometry
- “The Face of Time: Dial Manufacture at Glashütte Original,” Time and Watches
- “Savoir-Faire, Chapter Two: Discover how our watch-cases are made,” TAG Heuer Magazine
Thanks for reading this.